Direct manufacturer deployment of specialized liquid containment, temperature-stable cargo reefers, and certified heavy-duty bulk freight equipment.
Navigating modern chemical transportation requires strict adherence to international safety matrices, advanced metallurgical engineering, and resilient supply chain workflows.
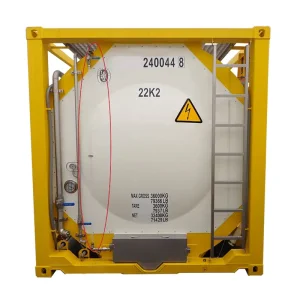
Global regulatory bodies demand zero-defect manufacturing for bulk chemical transport. From Class 3 flammable solvents to Class 8 corrosive acids, containers must mitigate hydraulic surge, extreme thermal fluctuation, and catastrophic rupture risks through precision relief valves, robust baffles, and ASME VIII-certified construction.
Global logistics hubs are aggressively phasing out single-trip flexitanks and intermediate bulk containers (IBCs) in favor of reusable, intermodal ISO tank containers and custom-lined chemical freight modules. This transition cuts operational carbon emissions by up to 38% and minimizes product contamination risks across intermodal corridors.
The rise of high-purity electronics chemicals, pharmaceutical intermediates, and specialized petrochemicals has driven the need for advanced surface passivations, electropolishing, and fluoropolymer internal liners (PTFE/PFA) that prevent cross-contamination and micro-ion leaching during transoceanic transit.
Engineered to withstand the world's most aggressive operating environments, our container architectures adapt seamlessly to multi-climate logistics networks.
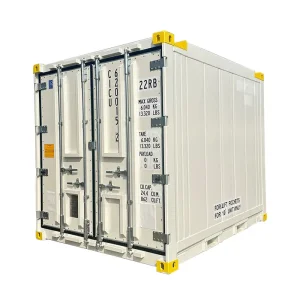
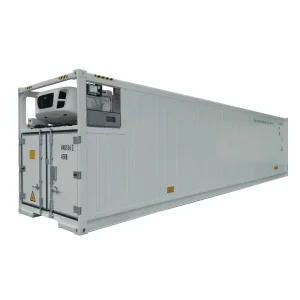
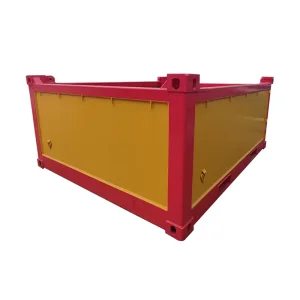
Engineered under DNV 2.7-1 / EN 12079 compliance matrices. Integrated 4-point dynamic lifting sling sets, low-temperature impact resistant corten structures, and Class A explosion-proof refrigeration components designed for high-salinity offshore drill ship servicing and chemical dosing supply chains.
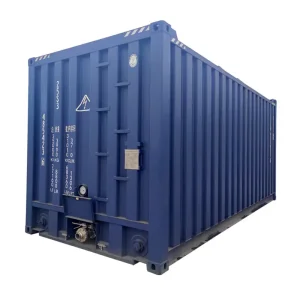
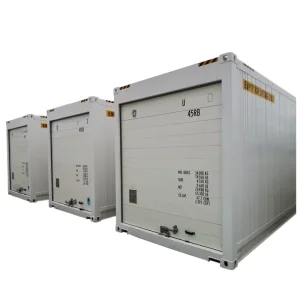
Heavy-duty, vacuum-tested liquid containers optimized for bulk pesticide, fertilizer intermediate, and bulk solvent distribution across inland rail and unpaved hinterland transport routes. Featuring enhanced rollover protection, automated pressure vents, and sediment-preventing bottom outlet configurations.
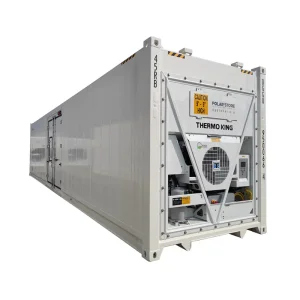
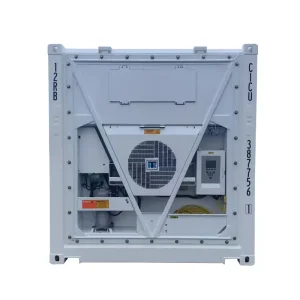
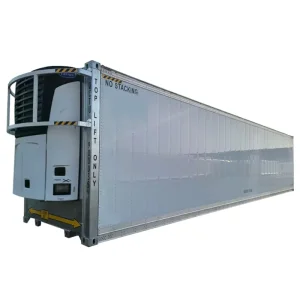
Ultra-clean 316L stainless steel containers and reefer modules equipped with Carrier, Daikin, or Thermo King refrigeration units. Guarantees precise temperature regulation (+/- 0.25°C) to prevent phase separation, degradation, or thermal expansion of photoresists and sensitive bio-precursors.
Positioned within strategic industrial manufacturing clusters in Tianjin and Suzhou, our manufacturing hubs integrate vertically from base metallurgical processing to rapid maritime deployment.
Operating just 100 kilometers from Tianjin and Suzhou deepwater maritime facilities drastically reduces drayage expenses and eliminates inland logistics bottlenecks. Our automated submerged-arc welding lines, automated high-pressure hydro-testing chambers, and proprietary anti-corrosion coating workshops ensure that every chemical and freight module delivered surpasses international CSC, TIR, and ISO standards with industry-leading turnarounds.
Comprehensive technical breakdown for procurement engineers and logistics portfolio directors.
| Module Category | Primary Metallurgy / Shell | Thermal & Pressure Rating | Certified Standard | Typical Industrial Media |
|---|---|---|---|---|
| ISO Chemical Tank Container (20ft) | Stainless Steel 316L / Titanium Alloy Option | Working: 4.0 Bar | Test: 6.0 Bar (-40°C to +130°C) | IMDG, ASME VIII, ADR/RID, BV, CSC | Solvents, Corrosive Acids, Lubricants, Organics |
| Offshore Reefer Container (DNV 2.7-1) | Corten High-Tensile Steel + Marine Zinc Coating | -30°C to +50°C Controlled Delta | Thermal Barrier | DNV 2.7-1, EN 12079, ISO 1496-2 | Refrigerated Chemical Dosing, Offshore Food Stores |
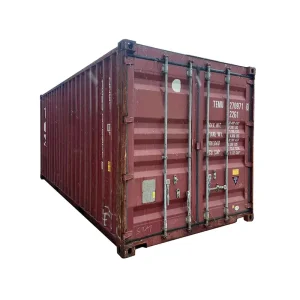
| High-Cube Controlled Insulated Unit | Anti-Corrosive Corten Structural Skeleton | Polyurethane High-Density Thermal Core | ISO 1496-1, TIR, BV Quality Approved | Bulk Chemical Drum Storage, Agrochemical Dry Goods |
| Intermodal Rail/Road Enclosure | Structural High-Tensile SPA-H Weathering Steel | Standard Atmospheric / Ambient Dynamic Shift | UIC, Belt & Road Compliant, ISO 668 | Battery Packs, Chemical Feedstocks, Raw Polymers |
The next generation of chemical containerization is smart, sustainable, and data-integrated.
Integration of solar-powered ATEX Zone 1-certified IoT sensor packages. Transmitting real-time GPS coordinates, ullage cavity pressure, ambient and core cargo temperatures, and lateral dynamic shock load warnings directly to ERP hubs worldwide.
Adoption of low-VOC, zero-solvent ceramic waterborne thermal reflective coatings. Combined with recycled alloy substrate frames and green steel alternatives, our next-generation units reduce production lifecycle emissions by 25% while boosting chemical corrosion resistance.
Engineered internal sanitary wash nozzles and self-draining geometric bases accelerate cleaning turnaround cycles between differing hazardous classes, reducing turnaround time from days to mere hours at maritime cleaning depots.
Procuring industrial chemical equipment demands frictionless engineering sign-offs, verified regulatory stamps, and responsive post-delivery servicing.
From non-standard footprint modifications to side-discharge valve manifolds, roll-up shutter configurations, and specialized interior floor lashing points, our engineering division crafts custom technical drawings within 24 hours.
Every container leaves our facility accompanied by a full traceability file: raw material mill test certificates (MTC), non-destructive testing (NDT) reports, third-party Bureau Veritas (BV) certificates, and DNV test validations.
For active temperature-controlled chemical containers, we standardize on global refrigeration market leaders: Carrier Transicold, Thermo King, and Daikin. This ensures immediate local access to factory-trained technicians and spare components in 120+ nations.
Browse our verified portfolio of offshore cargo baskets, refrigerated modules, liquid containment units, and modular prefab structures.
Actionable answers addressing certification, metallurgy, bespoke customization, and shipping logistics.
Our standard production lines deliver 10ft, 20ft, 20ft High Cube, 40ft, and 40ft High Cube containers. For liquid chemical containment, we offer standard 20ft ISO frame designs ranging from 14,000 to 26,000 liters. Specialized modules, including side-open door reefers, roll-up configurations, half-height ore bins, and offshore skids, are built to customer project drawings.
All CIMIC manufacturing processes are certified under the ISO 9001 Quality Management System. Our maritime cargo containers hold Bureau Veritas (BV) classification approvals, guaranteeing full compliance with CSC (International Convention for Safe Containers). Specialized offshore modules are rigorously manufactured to DNV 2.7-1 and EN 12079 criteria, and liquid chemical tanks adhere directly to IMDG, ASME VIII, and ADR/RID requirements.
We partner directly with leading industrial refrigeration manufacturers, including Thermo King, Daikin, and Carrier Transicold. This ensures clients can choose unit machinery compatible with their regional maintenance networks, ensuring instant access to authorized field service engineers, diagnostic software, and certified OEM spare parts.
Yes. Approximately 45% of our annual manufacturing output comprises bespoke OEM and ODM orders. Our engineering division collaborates directly with your technical personnel to adjust shell alloys (316L, 304, or carbon corten), apply specialized internal fluoropolymer or phenolic anti-corrosive coatings, customize valve manifold connections, and reinforce structural points for high-density payloads.
New custom and standardized builds are manufactured at our primary production facilities in Tianjin and Suzhou, strategically located within 100 kilometers of deepwater shipping berths. This short distance enables swift vessel loading and cost-effective ocean freight. For clients seeking immediate container solutions, we also maintain fleets of inspected used containers positioned across major Chinese hub ports.
Standard ISO-dimension containers and stocked items feature flexible ordering starting at 1 unit. For fully bespoke engineered chemical or offshore units, our engineering team evaluates production efficiency to provide an optimal batch schedule. Inquiries submitted via our portal receive an itemized technical quote and dimensional blueprint within 24 business hours.